-
What is the biggest ABB VFD buying mistake to avoid?
-
How do I get ABB VFD tech support without being an engineer?
-
What drive compliance requirements should I verify before buying ABB VFDs?
-
Is it smart to combine a bulk safety PLC order with ABB VFD purchases?
-
Does the contactor distributor matter when I'm buying ABB VFDs and controls?
-
Is the cheapest ABB VFD option ever the right choice?
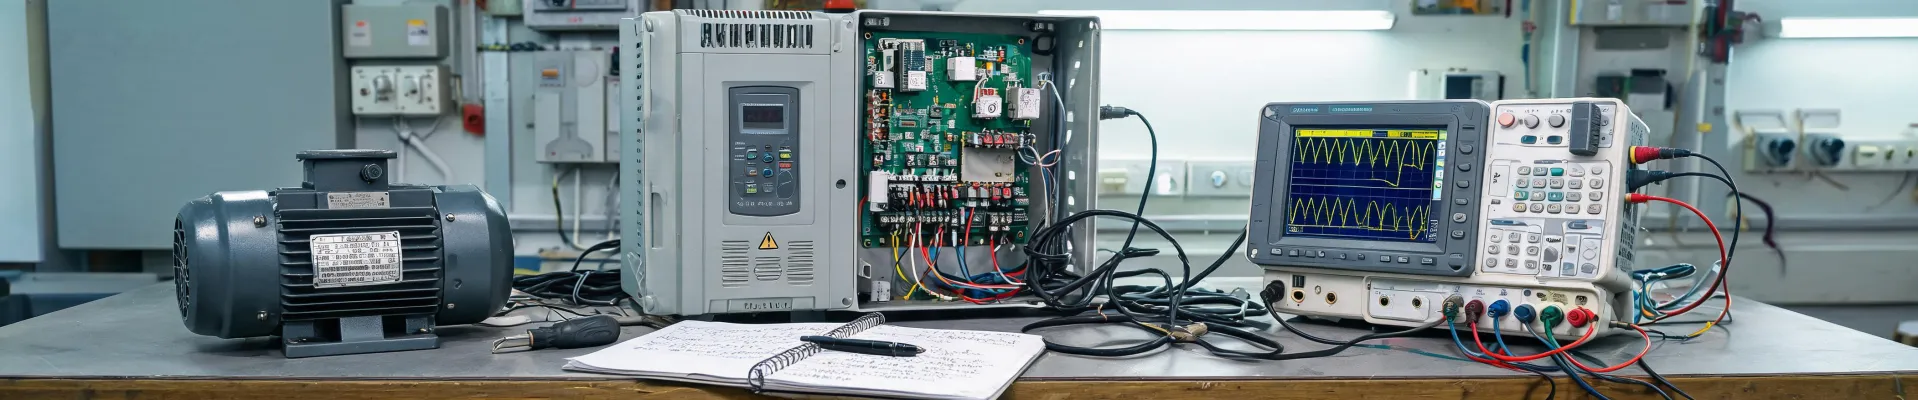
If you're the person who has to buy ABB VFDs and related control components—but you're not the engineer who will actually wire them in—this one is for you. I'm a purchasing administrator, not an electrical engineer. Since 2020 I've managed roughly $400,000 a year in control-component buying for a 180-person manufacturing company across eight vendors. I've made mistakes, and I've learned how much good distribution and documentation matter.
Here are the questions I keep running into, along with the answers that would have saved me time if I'd understood them earlier.
What is the biggest ABB VFD buying mistake to avoid?
The conventional wisdom is that a VFD is a VFD. In practice, the part number is the product. Thinking that every ABB VFD part number with the same base model is the same drive is a dangerous shortcut. It's not. One part number can include a different degree of protection, optional control panel, EMC filter, or fieldbus adapter. The price difference between two versions may be small; the reorder and downtime pain is not.
I've seen order placements go sideways because someone grabbed a listing that said ACS880 without checking the full catalog number. Then the drive arrives and does not match the panel drawing. The drive itself is fine. The product is wrong for the project.
If you handle purchasing, ask the engineer for the complete part number, not the model family. If you're using an online distributor, filter by the exact ABB type code—and ask the distributor to confirm it before shipping.
How do I get ABB VFD tech support without being an engineer?
You can call ABB tech support, but they are a lot more effective when you give them something to work with. I'm not the application expert, so I prepare a small file before contacting support:
- the exact drive series and type code
- the firmware version shown on the panel
- a photo of the fault code or the message displayed
- the motor nameplate info (even if I don't understand half of it)
- a one-line explanation of the machine operation
That last one is what most people skip. 'Drive won't run' is a support dead end. 'Drive runs a 5 HP fan motor, faults at 30 Hz, and there's a brake resistor installed' gets a much better answer.
This gets into application territory that isn't my expertise. If we have a complicated motor circuit problem, I involve our plant engineer. What I can tell you from a procurement perspective: ABB tech support can help if you bring them the right information. They cannot help if your paperwork is 'I think it is an ABB VFD.'
(As of early 2026, at least.)
What drive compliance requirements should I verify before buying ABB VFDs?
This one had to bite me before I believed it. I once accepted a compliance certificate from a distributor because the main brand name matched the drive—but the model number on the certificate didn't match the drive we ordered. The panel was ready to ship, and the inspector spotted it. We ate the delay.
For ABB variable frequency drives in North America, verify the drive is listed to the proper standard—typically UL 61800-5-1 or a current equivalent. An inspector or Authority Having Jurisdiction may look for the listing marking on the nameplate. The installation also generally needs to follow the National Electrical Code requirements that apply to motor control equipment, and your local electrical code may add more.
If you're shipping to the EU or UK, the CE mark alone is not the final word. The drive has to be covered by a Declaration of Conformity for the exact model, and it should align with the Low Voltage Directive and EMC Directive. For safety-related functions, the ABB drive's safety data must be used in a way that supports the machine's functional safety calculations. This is where a bulk safety PLC implementation and the drive's Safe Torque Off parameters need to be treated as one system, not two separate components.
I do not try to interpret those safety sheets myself. I make sure the supplier provides the valid documentation, and I send it to our engineer for review.
Is it smart to combine a bulk safety PLC order with ABB VFD purchases?
From a purchasing administration point of view, yes, if you have a defined project and an integrator or engineer who can manage firmware versions. Bundling safety PLCs with drive components can reduce shipping, consolidate paperwork, and make it easier to get a consistent answer from one supplier.
But a safety PLC is not a commodity. It comes with different I/O modules, communication options, and firmware. If you order extra CPUs just because 'bulk safety PLC' pricing looks good, they may sit on the shelf for a year. By the time you need them, the firmware may be old, and your integrator may not want to swap them into a running machine.
Looking back, I should have confirmed the CPU quantity with our integrator before placing a bulk order. I didn't, and one CPU became obsolete before we used it. Not a catastrophic mistake, but it turned a 'savings' into a shelf ornament.
This approach works for us because our projects are driven by a main line expansion and we buy in predictable batches. If you're buying for occasional repairs or one-off machines, I'd probably order per project instead of in bulk.
Does the contactor distributor matter when I'm buying ABB VFDs and controls?
It matters more than people think. A contactor looks simple, but you need the coil voltage, contact rating, utilization category, and auxiliary contact configuration to line up with the machine design. A good contactor distributor asks about those details. A bad one just takes the order and ships the cheapest item with a matching model prefix.
For ABB VFD installations, I like having one distributor who can handle the drives and the contactors separately, but who still understands the relationship between them. When the engineer changes a 24V DC coil scheme, I don't want to chase a different supplier for 50 contactors.
You do not necessarily need every contactor to be an ABB part. But you do need a distributor who can cross-reference ratings honestly. The extra few minutes spent confirming the coil voltage saves a call from the panel shop later.
Is the cheapest ABB VFD option ever the right choice?
If it genuinely meets the application, yes. Cheapest is not automatically wrong. But cheapest as a shortcut usually is.
I've seen the pattern where the lower-priced drive with a similar base model had fewer I/O, no integrated EMC filter, or a control panel option that didn't support what operations wanted. It looked like a bargain on the purchase order. Then the engineer had to add accessories, enclosures, or adapter kits. Add labor and lead time, and the 'cheap' drive ended up costing more than the one on the spec.
Quality perception is part of this too. If you are building a machine that your own customers will see, the components inside affect their confidence in your product. That does not mean pay for anything unnecessary. It means don't make a decision based only on the line item.
When we standardized on ABB drives for the main production line, drive-related downtime did drop. I cannot tell you to expect the same result in every situation. But I can tell you that one bad selection can cost more in labor and lost production than the component itself.
Rebecca Sloan
Rebecca Sloan is a power distribution and protection analyst specializing in circuit breakers, switchgear, contactors, fuses, surge protective devices, and coordination. She applies IEC 60947-2 breaker requirements, IEC 60269 fuse characteristics, and IEC 61643-11 tests while examining rated voltage, breaking capacity, time-current curves, selectivity, and prospective short-circuit current. She helps engineers and buyers compare protective devices against documented fault levels, installation conditions, maintenance access, and continuity priorities.