-
The Order That Looked Perfect on Paper
- You Think the Problem Is the Product. It Isn't.
- The Relay Supplier Trap: Why Bulk Orders Fail Differently
-
Evaluating Safety PLC Manufacturers: Beyond the Brand Name
-
The Real Cost of "Compliant" Failures
-
How to Close the Gap (Without Rebuilding Your Entire Procurement Process)
-
What I Wish I'd Known Five Years Ago
The Order That Looked Perfect on Paper
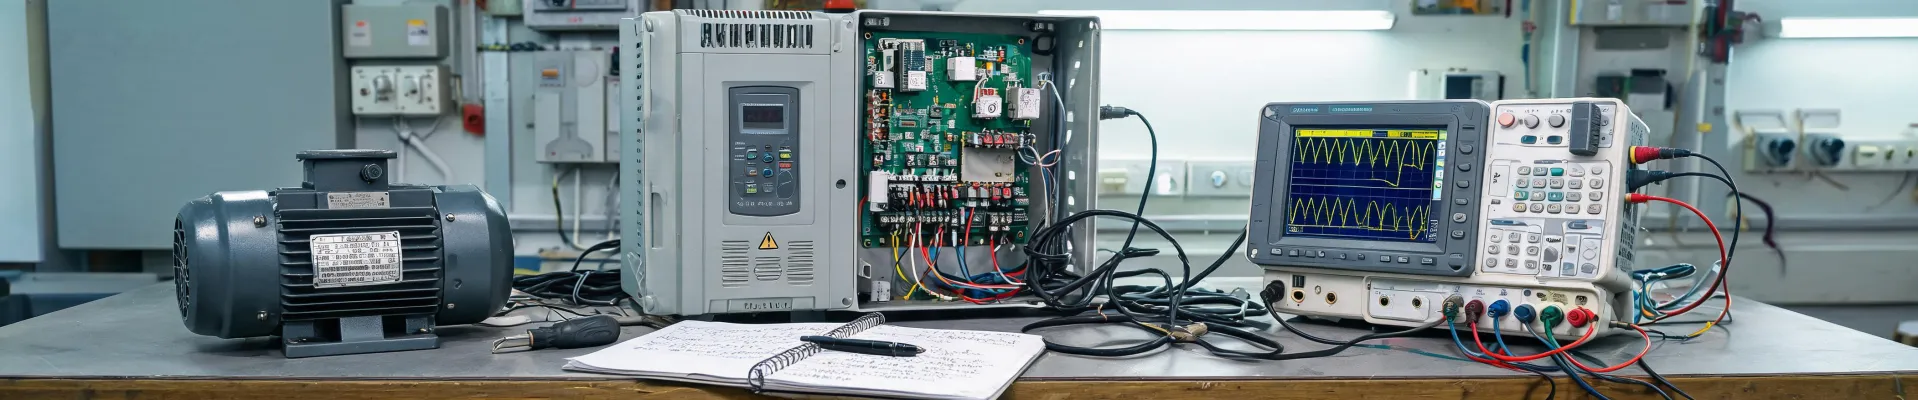
In Q1 2024, we installed 40 ABB VFD drives on a packaging line. All 22kW class. All sourced from a certified distributor. All with full CE and UL documentation. Incoming inspection passed. First startup passed. Then, on the third shift under load, four of them tripped on F0007 — DC bus overvoltage.
We scoped it. The deceleration curve didn't match what we'd specified. The vendor insisted the drives were exactly to spec. From their side, they were. The firmware revision interpreted our ramp parameters differently than the previous generation. Nobody on our procurement team caught it, because nobody knew to ask.
That scenario has played out in variations at least a dozen times over four years. As a quality and brand compliance manager at a systems integration company, I review roughly 200 unique SKUs annually before they reach our customers. In 2024, we rejected about 18% of first deliveries — not because the products were defective, but because the definition of 'compliant' didn't match between the vendor and us.
You Think the Problem Is the Product. It Isn't.
Most procurement teams think their process is fine. Pick a source, verify the part number against the datasheet, confirm certifications, place the order.
That's the surface problem: "The vendor sent the wrong model" or "The part doesn't meet spec."
But here's what I've learned from rejecting hundreds of batches: specification sheets describe what a component can do. They don't describe what it will do in your specific application, in your specific panel, under your specific load profile.
The gap between those two things is where nearly every quality failure lives.
The 'ABB VFD Support' Assumption That Costs You Weeks
When you buy an ABB VFD, you're also buying access to support. But whose support? The distributor's order desk, or an engineer who has actually commissioned drives on a panel like yours?
I assumed those were the same thing. Didn't verify. Turned out the distributor we were using had zero field engineers on staff — they relayed every technical question back to ABB's factory support, which added 5-7 business days to every loop.
For a drive fault code that's halting production, that's not support. That's a ticket queue.
What most people don't realize is that ABB VFD support quality varies enormously by channel. The manufacturer's technical documentation is consistent. The interpretation of that documentation is not. A distributor that stocks drives as a line item is not the same as one that stocks them as a specialty.
Now I ask a single question before qualifying any ABB VFD source: "How many of your staff have commissioned an ACS880 on a live panel in the last 12 months?" If the answer is vague, I move on.
The Relay Supplier Trap: Why Bulk Orders Fail Differently
Relays seem simple. They're mechanically and electrically well-understood. So why do bulk relay orders cause so many headaches?
Because the failure mode isn't in the sample you test. It's in the batch consistency you don't.
In 2023, we received a batch of 2,000 electromechanical relays from a relay supplier we'd used before. AQL sampling passed — 0.4% defect rate, well within tolerance. Three months later, eight units in the field had contact resistance drift that exceeded the datasheet's end-of-life specification. Not at end of life. At 40% of rated cycle count.
The vendor's response was predictable: "The sampled units passed. Your field conditions must be outside our assumptions."
That's how it usually goes. And it's frustrating, because they're technically correct about their sample. The problem is that AQL sampling can't catch batch-level process drift.
What Changed Our Relay Verification Process
After that incident — which cost us roughly $22,000 in field replacements — we added a step that none of our relay suppliers expected: we now request temperature-cycled production samples from the actual manufacturing lot, not just from distributor stock. We test contact resistance at -20°C, 25°C, and 70°C.
For a bulk relay order of 1,000 units, this adds about $400 and two weeks. It has caught three process issues across five relay suppliers in two years.
Here's something vendors won't tell you: the relays from a single manufacturer can differ meaningfully between production runs — especially for general-purpose relays where the coil wire gauge or contact plating can shift based on raw material availability. "Same part number" doesn't mean "same batch behavior."
Evaluating Safety PLC Manufacturers: Beyond the Brand Name
When people ask how to evaluate safety PLC manufacturers, they usually want a comparison chart. Brand A vs. Brand B. Price per channel. Certification list.
But evaluating a safety PLC manufacturer isn't a product comparison. It's a system assessment.
That's a distinction most procurement teams miss entirely.
Here's what actually matters, and it's rarely on the spec sheet:
1. Certification scope, not just certification. A TÜV certification for a product family doesn't automatically cover every model in that family. I've seen safety PLCs where the SIL 3 certification applied to the CPU module but not the I/O modules — and the I/O was exactly what our customer's process needed. The manufacturer wasn't lying. They were accurately describing a certification that we had misread.
2. Diagnostic coverage transparency. Any safety PLC manufacturer can claim SIL 3. The useful question is: what diagnostic coverage do they publish, and at what proof test interval? Some manufacturers provide detailed FMEDA data. Some don't. If the data isn't available before purchase, assume it won't be available during commissioning either.
3. Toolchain lock-in depth. The programming environment determines how much re-engineering is needed when you switch hardware — or when you need to integrate with legacy systems. A manufacturer whose safety PLCs ONLY program in their proprietary environment has you locked in. That's not necessarily disqualifying — but it IS a cost you need to price in upfront.
If you're wondering how to evaluate safety PLC manufacturers, start by defining what your process actually requires and work backward. I've watched teams choose the most recognized brand and then spend months redesigning I/O architecture because the certified diagnostic response time didn't match the machine's actual safety reaction budget.
The Real Cost of "Compliant" Failures
The ABB VFD failures cost us a week of production downtime at the customer's facility. The relay batch cost $22,000 in field replacements plus a customer confidence hit that took two quarters to rebuild. The safety PLC mismatch cost six weeks of redesign and a postponed audit.
None of these were product defects. All of them were evaluation failures.
When I compared our units processed through the improved verification protocol versus our older process, the difference wasn't subtle. Our field failure rate dropped from 4.2% to under 1%. On a 50,000-unit annual order value, that's the difference between chasing warranty claims and building reference accounts.
I get why teams default to the cheapest quote or the most famous brand. Budgets are real, and nobody gets fired for choosing the market leader. But the hidden cost of inadequate evaluation rarely shows up in the purchase order. It shows up in the maintenance log, the customer complaint, and the contract renewal that doesn't happen.
How to Close the Gap (Without Rebuilding Your Entire Procurement Process)
I'm not going to tell you to rebuild everything. Here's what worked for us, in order of impact:
For ABB VFD sourcing: Ask one question — who commissions these drives, and when did they last do it? If you can't get a clear answer, find another source. Technical support is worth more than a 3% price difference.
For relay suppliers: Request temperature-cycled samples from your production lot before approving bulk shipments. It's a small cost that catches process drift AQL sampling can miss. For critical applications, ask for batch traceability data — if the supplier can't provide it, that tells you something about their process control.
For safety PLC evaluation: Map certification scope to your actual modules. Request FMEDA or diagnostic coverage data before purchase. And price in the toolchain risk. The evaluation starts with your safety requirements, not the manufacturer's catalog.
To be fair, all of these steps add time and cost to the procurement cycle. I'm not going to pretend they're free. But every single one of them has paid for itself within the first year — usually within the first project.
I'm not 100% sure this framework will work for every product category. Some applications are genuinely low-stakes, and "verify everything" is overkill. Call it — if the failure cost is low and the recovery is fast, standard AQL processes are probably fine.
But if a field failure means a production line stops, a safety audit fails, or a customer walks — the evaluation gap is where your quality actually lives. Not in the product. In how you chose it.
What I Wish I'd Known Five Years Ago
After five years of managing component quality across drive, relay, and safety PLC categories, I've come to believe that the 'best' source is meaningless without the 'best' evaluation process. The product doesn't fail you. The process does.
ABB VFD drives are solid products. So are most relays. And the safety PLC market has multiple manufacturers with genuinely strong portfolios. The problem was never them.
The problem was me, assuming I could evaluate all three categories the same way. A drive isn't a relay. A relay isn't a safety PLC. Each requires different rigor, different questions, and different tolerances for uncertainty.
Define your requirements. Verify the specificities. Ask the uncomfortable questions before you sign, not after you install.
That's the whole lesson. It took about four years and several expensive rejections to learn it — but it's the one thing I'd put in every procurement training manual if I could.
Rebecca Sloan
Rebecca Sloan is a power distribution and protection analyst specializing in circuit breakers, switchgear, contactors, fuses, surge protective devices, and coordination. She applies IEC 60947-2 breaker requirements, IEC 60269 fuse characteristics, and IEC 61643-11 tests while examining rated voltage, breaking capacity, time-current curves, selectivity, and prospective short-circuit current. She helps engineers and buyers compare protective devices against documented fault levels, installation conditions, maintenance access, and continuity priorities.