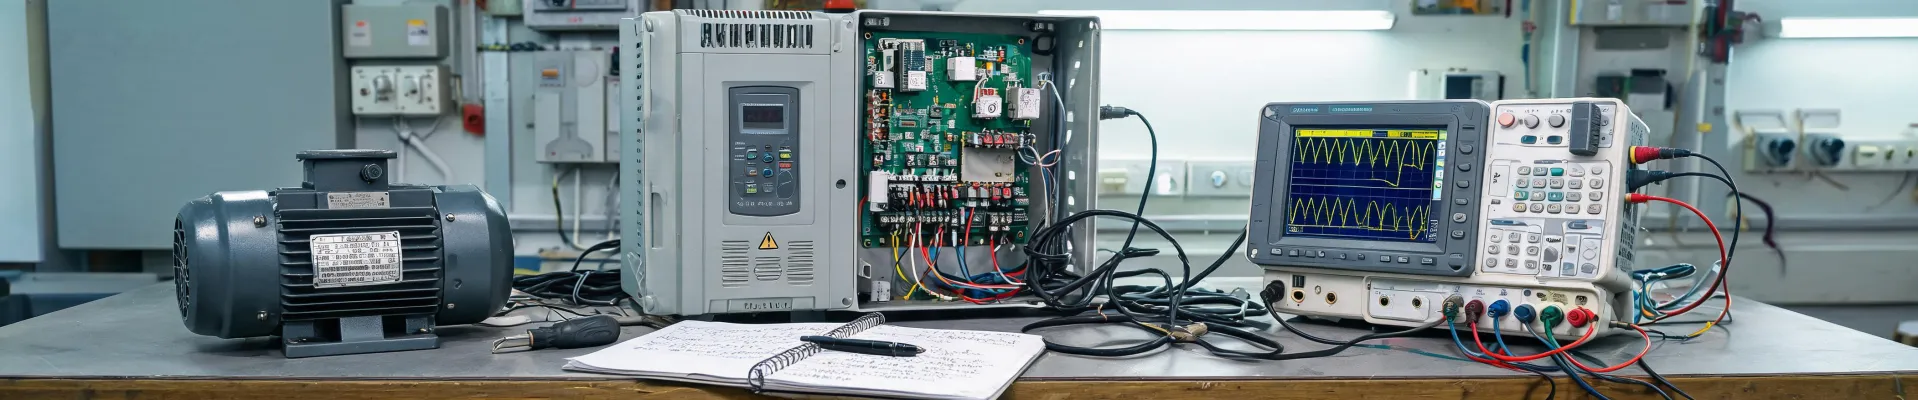
-
1. Match the VFD to the Motor's Full Nameplate—Not Just Horsepower
-
2. Confirm Environmental Conditions Before Choosing an Enclosure
-
3. Trace Every Signal Path—Analog and Digital
-
4. Select Contactors by Utilization Category, Not Just Rated Current
-
5. Audit the PLC's I/O and Protocol Map with 20% Headroom
-
6. Verify Safety Functions and Certification Compliance
-
7. Document Everything—Including the Firmware Version
-
Five Common Spec Mistakes We See Repeatedly
I'm the quality and brand compliance manager at an industrial controls distribution company. Every day, I review specifications that go into customer orders—roughly 200+ unique items a year. In Q1 2024, I rejected 11% of first deliveries because specs didn't match what was actually needed. Not because the parts were defective. Because the specifications were wrong from the start.
Over four years of this work, I've put together a 7-point checklist that we run on every ABB VFD and control component order before it goes to the warehouse. It takes about 30 minutes to work through. It saved us from a $22,000 redo that would've happened if I hadn't caught a contactor mismatch.
Use this when you're specifying or ordering ABB VFD drives, relays, PLCs, contactors, or any associated control components.
1. Match the VFD to the Motor's Full Nameplate—Not Just Horsepower
This is the one I see most often. An engineer looks at a motor's HP rating and picks a VFD with the same horsepower. That's a starting point, not a specification.
Pull the full nameplate data from the actual motor. You need:
- Rated current (FLA) at the operating voltage
- Speed range and base frequency
- Overload capability and duty cycle
- Insulation class, and whether the motor is inverter-rated
What most people don't realize is that a 10 HP motor at 460V doesn't draw the same current as a 10 HP motor at 230V. I've seen orders where the VFD was correctly sized for horsepower but undersized for the motor's actual full-load amps at the site's voltage. The drive tripped on overcurrent within the first week.
Checkpoint: The VFD's rated output current should be at least 110% of the motor's full-load current for normal duty, and more for heavy-duty applications.
2. Confirm Environmental Conditions Before Choosing an Enclosure
I can't count how many times a drive has been flagged as "NEMA 1" when it's going into a washdown area or an outdoor location with high humidity. You don't need to memorize the whole NEMA/IP table. But you do need to know:
- Maximum and minimum ambient temperature at the installation site
- Humidity range, including condensation possibilities
- Altitude (above 1,000 meters, derating applies)
- Whether dust, oil mist, or washdown chemicals are present
Here's something vendors won't tell you: a VFD with a higher IP rating in the same product family isn't always just "the same drive in a tougher box." Derating curves can differ. Cooling effectiveness changes. If you need IP54 or IP55, confirm the current rating at your ambient temperature from the manufacturer's official derating tables—not from the brochure.
3. Trace Every Signal Path—Analog and Digital
We had a situation two years ago where we ordered a batch of VFDs and PLCs for a packaging line. The engineer on site said the PLC should "communicate with" the drives. We said "sure, we'll set up Modbus RTU." What we didn't catch is that the site's PLC was using Profibus DP, not Modbus. Both are standard. Both speak serial communication. Not the same thing at all.
We discovered this when the commissioning engineer couldn't get a single status register to show up. Result: two weeks of schedule delay and a rushed gateway purchase that cost more than the PLC itself.
Before you place the order, write down every signal path:
- Analog input to the VFD: 4-20mA current loop or 0-10V DC?
- Digital commands: source and voltage (24V DC sink/source)
- Communication protocol: Modbus RTU, Profibus, EtherNet/IP, Profinet?
- Feedback signals from the drive back to the PLC
Checkpoint: Put the communication protocol in writing and confirm it with whoever is programming the PLC. I don't care how senior they are. Get it in an email.
4. Select Contactors by Utilization Category, Not Just Rated Current
Contactor specifications seem simple until they aren't. The rated current printed on the front is only meaningful when you know the utilization category it relates to.
Per IEC 60947-4-1, contactors are categorized by what they're switching:
- AC-1: Non-inductive or slightly inductive loads
- AC-3: Squirrel-cage motors—starting and switching off during running
- AC-4: Squirrel-cage motors—starting, plugging, and inching
Here's the thing: a contactor rated 25A in AC-1 might only be rated 18A in AC-3. I rejected a batch of 200 contactors in 2023 because the vendor quoted "25A contactors" and we needed AC-3 duty—the actual AC-3 rating was below the motor's full-load current.
Also check that the coil voltage matches your control circuit. This sounds obvious, but you'd be surprised. 24V DC coils and 110V AC coils look identical from the outside on many models.
5. Audit the PLC's I/O and Protocol Map with 20% Headroom
The mistake I see with PLC specifications is almost always the same: undersized I/O, or exactly enough I/O with zero room for change.
When you're putting together the PLC specification:
- Count digital inputs and outputs for current needs
- Count analog inputs and outputs (voltage vs. current—not always interchangeable without jumpers)
- Check available communication ports (serial, Ethernet, fieldbus options)
- Add 20% spare capacity for each
Why 20%? Because every control panel gets at least one "small addition" during commissioning. It's almost a law. When we implemented our 20% headroom policy in 2022, our on-site modification rate dropped by roughly a third.
Checkpoint: If the PLC spec leaves zero unused I/O on the main CPU, it's wrong. Revise it.
6. Verify Safety Functions and Certification Compliance
Modern ABB VFD drives include standard safety functions like STO (Safe Torque Off). But there's a difference between the hardware supporting STO and the system actually being safety-certified for your application's required performance level.
Ask yourself:
- Does the drive have STO as standard, or is it an option?
- What's the safety integrity level (SIL) or performance level (PL) rating?
- Do your safety relays or safety PLCs integrate properly with the STO input?
- What's the certified stopping time for the drive in your configuration?
Per IEC 61800-5-2, safety functions for adjustable speed drive systems have defined behavior and response times. Your system integrator should be able to show you the relevant Declaration of Conformity—not just say "it has STO."
I'd also check that the drive's EMC filter configuration matches your installation. IEC 61800-3 covers EMC requirements for power drive systems, and the filter setup affects both compliance and motor cable length limits.
7. Document Everything—Including the Firmware Version
This is the step most people skip, and it's the one that creates the most headaches later. Here's what happened to us:
We once received a VFD that was functionally identical to the previous batch. Same model, same power rating. But the firmware version was older, and it didn't support a Modbus register the commissioning engineer needed. Nobody had recorded what firmware version the earlier drives came with. The engineer spent two days troubleshooting "communication problems" that were actually a firmware mismatch.
Now, every order in our system includes:
- Product model and type code, photographed and archived
- Firmware version noted at receiving
- A backup of the parameter set once the drive is configured
- Serial numbers recorded against the specific project
- Installer name and installation date
We didn't have a formal parameter backup process. It cost us two rush orders and a lot of embarrassment in 2021. The third time it happened, I finally created a verification protocol. Should've done it after the first.
Five Common Spec Mistakes We See Repeatedly
Before you finalize any ABB VFD or control component order, scan for these:
- HP-based VFD selection. Always select by motor full-load current and application duty.
- Using AC-1 contactor ratings for motor loads. Check the AC-3 rating.
- Mismatched analog signals. 4-20mA and 0-10V aren't interchangeable without module configuration.
- Communication protocol assumptions. It's not "PLC to VFD." It's the specific protocol and version.
- No documentation. Firmware, serial numbers, and parameter backups matter more than you think.
This checklist doesn't replace the manufacturer's technical manual. It does, however, replace the trial-and-error approach that costs money and delays projects.
If you're looking for ABB VFD tech support during specification, this checklist is a solid starting point—but always pair it with the official documentation for your specific drive series. The fundamentals haven't changed: you still need to match specs to the real load. But the execution has transformed. Tools like ABB's drive selection software make initial sizing easier than it was a decade ago. What they don't do is catch the site-level details—the actual motor nameplate, the washdown environment, the PLC protocol on site. That's still a person's job.
Rebecca Sloan
Rebecca Sloan is a power distribution and protection analyst specializing in circuit breakers, switchgear, contactors, fuses, surge protective devices, and coordination. She applies IEC 60947-2 breaker requirements, IEC 60269 fuse characteristics, and IEC 61643-11 tests while examining rated voltage, breaking capacity, time-current curves, selectivity, and prospective short-circuit current. She helps engineers and buyers compare protective devices against documented fault levels, installation conditions, maintenance access, and continuity priorities.